Never Approve a Sauce Filler on Cold Water Alone!
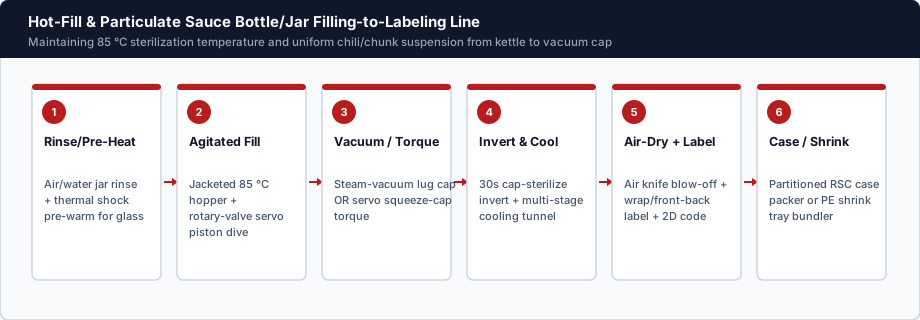
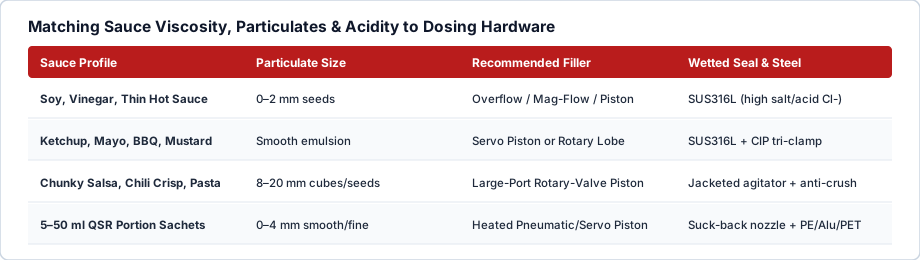
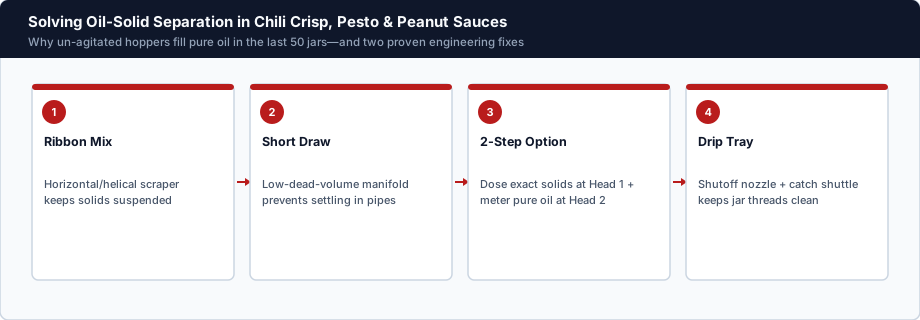
Cold tap water hides cavitation on 45,000 cP BBQ paste, stringing on sweet chili glaze, solid settling in chili crisp, and seal expansion at 85 °C! Grounded in sauce line sizing and guides and hot-fill viscosity and sanitary specs, insist on a heated viscous + particulate Factory Acceptance Test using food-grade CMC/xanthan gel, vegetable oil + chili/bean solids, or actual batch sauce.
Verify all six checkpoints below before authorizing ocean freight.
Six-Point Sanitary Sauce Line FAT Matrix
Quantitative acceptance tests executed prior to crating:
| FAT Checkpoint | Test Method | Pass Criterion |
|---|---|---|
| 1. Multi-Head Weight Cpk | Weigh 10 consecutive cycles across all nozzles (500 g paste) |
Within ±0.2%–0.5% (±1.0–2.5 g); Cpk >= 1.33 |
| 2. Solid-to-Oil Ratio | Drain & weigh solids from Jar #1, #100 & #300 (chili oil) |
Drained solid weight variance <= ±3% across batch |
| 3. Thread & Neck Cleanliness | Inspect 100 filled jars under UV/bright light before capper | 0 sauce drops on exterior neck threads; clean drip tray |
| 4. 85 °C Thermal & Seal Hold | Circulate 85–90 °C heated media continuously for 60 min | 0 PTFE piston/spool leaks; hopper holds ±1.5 °C |
| 5. Vacuum Lug Integrity | Cool 30 steam-capped glass jars to 30 °C; pierce w/ gauge | 35–55 kPa internal vacuum; 100% dud-detector reject test |
| 6. Timed Sanitary Strip/CIP | Flush CIP manifold + strip 1 cylinder/rotary valve by hand | Full tool-free strip & reassembly <= 15 minutes |
Inspect our SUS316L machining and wet-trial process on sauce packaging machine manufacturer.
Sanitary Sauce & Hot-Fill Notes
- Verify SUS316L With Handheld XRF Analyzer: Confirm
2.0%–2.5% Molybdenum (Mo)content on hoppers, pistons, rotary spools, and diving nozzles during FAT—separating genuine SUS316L from SUS304 instantly. - Test Worst-Case Squeeze Bottle Stability: Empty top-heavy inverted PET squeeze bottles tip easily at conveyor transfers—run 200 empty + filled squeeze bottles at 115% line speed to verify guide rails and pucks.
- Save Per-Nozzle Servo Calibration Offsets: Export touchscreen recipe backups recording dive stroke mm, bottom-up rise curve, suck-back delay, and agitator RPM.
Book Your Viscous & Hot-Fill FAT Session
Send your sauce specs and container samples via Project Brief.
Explore related condiment systems in Sauce Packaging Machines, Hot-Fill & Viscosity Specs, or send your viscosity, chunk mm & BPH via Project Brief.